
Quick Answer
A PPAP Level 3 documentation package for a custom OBD cable assembly normally contains a ballooned drawing, dimensional results for every populated cavity, a process flow diagram, PFMEA, control plan, MSA, material certificates, initial process studies, qualified lab reports, and a signed PSW. The OBD-specific proof that matters most is crimp height Cpk, pull force per terminal, full pin-to-pin continuity against SAE J1962, and revision traceability across every document in the submission.
A harness supplier ships a PPAP binder for a custom OBD-II cable assembly. The PSW is signed. The samples arrive in labeled bags. The dimensional report shows all 16 cavities within tolerance. Four weeks later, the OEM’s SQE opens the control plan and finds that the crimp height windows were copied from a different terminal family. The pull-force data came from a 22 AWG setup, but the production drawing calls for 20 AWG. The submission looked complete. It was not.
That mismatch is not a filing problem. It means the PPAP describes a process the factory has not yet shown it can repeat at volume. For an OBD cable, the gap usually appears in two numbers: crimp height and pull force per populated cavity. A 16-pin J1962 connector may have only 8 populated cavities, but each one is a separate crimp interface. If the PPAP does not prove each interface, the approval rests on a sample, not a process.
What follows is how the package reads at an SQE’s desk, not how it reads in a sales folder. It covers the documents that carry weight, the data that gets a Level 3 submission approved, the failure points that trigger re-submission, and the questions a buyer should ask before accepting a PPAP package. The focus is on evidence, not definitions.
What Does a PPAP Level 3 Package for a Custom OBD Cable Actually Contain?
A PPAP Level 3 is not one file. It is a package that ties design, process, measurement, and material evidence together. For a custom OBD cable assembly, the package usually contains:
- Design records, including the released drawing and a ballooned print.
- Dimensional results for the connector interface and cable assembly.
- Process flow diagram, PFMEA, and control plan.
- Measurement system analysis for crimp height and pull-force testing.
- Material and performance test records, including RoHS and REACH.
- Initial process studies, especially crimp height Cpk and pull-force capability.
- Qualified laboratory documentation, such as salt spray and flammability reports.
- Part Submission Warrant, signed against the production process.
- Sample parts from a production-intent run.
A PPAP package behaves like a chain. The SQE tests the weakest link first. A signed PSW with a dimensional report that does not trace back to the ballooned drawing is not a complete submission. It is a folder of files that will not survive an SQE review.
Design Records: A Ballooned Drawing Is the Anchor, Not a Formality
Before I open a dimensional report, I ask for the ballooned print. If the print is not ballooned, the report has no anchor. A 16-pin J1962 connector may have 8 populated cavities and 8 crimp interfaces. Without balloon numbers, you cannot tell which cavity was measured, which terminal was pulled, or which crimp setup produced the data. That is also where an ECU bench flashing OBD cable spec gap often starts: the drawing is one revision ahead of the process evidence.
Critical Design Record Callouts for OBD Cable Assemblies
For an OBD cable assembly, the design record has to define more than the overall length. The critical callouts are:
- Pin-to-pin assignment for all 16 cavities per SAE J1962, including which pins are populated, which are intentionally blanked, and whether the assembly uses Type A or Type B connector geometry.
- Wire gauge per circuit. A common OBD-II diagnostic cable uses 20 AWG for power and ground on pins 4, 5, and 16, and 22 AWG or 24 AWG for CAN lines on pins 6 and 14 and K-line on pin 7. If the drawing does not specify gauge by circuit, the SQE cannot verify that the crimp tooling matches the conductor size. The gauge choice also sets loop resistance; the test bench OBD cable AWG loop resistance ground separation discussion explains why that matters on a loaded bench.
- Shielding specification, if the assembly includes a shielded CAN pair. This includes the drain wire termination method: crimped to the connector shell, soldered to a ground pin, or left unterminated at one end.
- Connector orientation and keying, because a reversed housing can pass continuity but fail in the vehicle or test bench.
- Overmold material and color, if the assembly uses a custom overmold.
For older vehicles that still use K-line on pin 7, the same design record should reference the scanner protocol. A KWP2000 code explained K-line scanner note in the drawing package helps the SQE understand why that circuit is populated and why its resistance threshold differs from the CAN pair.
Revision Lock: The Most Common PPAP Rejection Point
A common rejection point is a revision mismatch. The drawing revision on the PSW does not match the revision on the ballooned print. This sounds trivial. In practice, it means the dimensional report, control plan, and PFMEA were all built against a different released drawing. The submission is technically incomplete even if the parts fit.
At factories I work with, every PPAP submission starts with a revision lock meeting. The quality engineer and the manufacturing engineer sit down with the released drawing and the BOM side by side. They confirm that the PSW, control plan, PFMEA, and dimensional report all reference the same revision level. If any document is one revision behind, the package does not leave the building.
What Does an SQE Check First on a 16-Pin J1962 Connector?
The dimensional report for an OBD cable assembly is not about measuring the cable length from end to end. It is about the interface. A 16-pin J1962 connector has a defined cavity geometry, terminal retention force specification, and mating dimension window. If the terminal is seated half a millimeter shallow, the pin may still make contact during a bench test but fail intermittently after 50 insertion cycles in the field.
A standard OBD2 male to female connector blue 16-pin diagnostic adapter can serve as a reference for the interface envelope, but the PPAP evidence must follow the released custom assembly drawing, not the catalog part. The same discipline applies whether the program uses an off-the-shelf adapter or a fully custom overmolded assembly.
Dimensional Report Table for a 16-Pin J1962 Connector
Here is what a production-intent dimensional report should contain for an OBD-II assembly:
| Measurement Point | Specification, Typical | Measurement Method | Why It Matters |
| Connector body width | Per SAE J1962 envelope | Caliper, 3 points | Ensures mating with vehicle-side receptacle |
| Cavity depth, terminal seated | Plus or minus 0.30 mm | Depth gauge, all populated cavities | Prevents intermittent pin contact |
| Overmold flash | 0.15 mm maximum | Visual plus pin gauge | Flash can block full insertion |
| Cable exit angle | 5 degrees maximum from axis | Protractor fixture | Excess angle stresses strain relief |
| Strain relief pull-out | 110 N minimum | Pull tester, 25 mm per minute | Prevents cable pullout from connector |
| Pin retention force per terminal | 50 N minimum for 0.22 mm squared | Pull test per USCAR-21 | Verifies crimp-to-terminal lock |
Why Pull-Force Data Per Cavity Matters
The pull-force row is where many submissions fail. A supplier will submit a single pull-force number, say 110 N, without specifying which terminal, which wire gauge, or which crimp setup produced it. An experienced SQE wants the raw data: five readings per terminal size, the crimp height used, the crimp width, and the conductor crimp pull-out values separated from the insulation crimp values. If the report shows one number with no supporting setup data, the submission is treated as a claim, not evidence.
For OBD cable assemblies specifically, the pin retention test should cover every populated cavity, not a sample. A 16-cavity connector with 8 populated pins has 8 individual crimp interfaces. The pull-force data must show that each one was verified during the first-article inspection. This is not overkill. It is the same discipline the OEM applies to its own harness suppliers.
Process Flow, PFMEA, and Control Plan: How the Documents Stay Linked
The process flow diagram for an OBD cable assembly looks simple: wire cut, strip, crimp, insert into housing, continuity test, overmold if applicable, final test, pack. The diagram itself is not the evidence. The revision number next to each step is.
A Level 3 submission requires that the process flow diagram, PFMEA, and control plan are interlinked. If the flow diagram says “Step 4: Crimp — Terminal A, Setup 001” and the PFMEA lists a failure mode for “wrong terminal used,” the control plan must specify the detection method: a terminal reel label scan, a crimp height measurement at setup, or a first-piece visual check with a boundary sample.
Three OBD-Specific PFMEA Failure Modes That Actually Matter
The PFMEA for OBD cable assemblies tends to focus on three failure modes that are specific to diagnostic cables.
Mis-Pinned CAN Lines
If pin 6, CAN High, and pin 14, CAN Low, are swapped during assembly, the cable may pass a continuity test that only checks for opens and shorts. The harness will power up the diagnostic tool, but the CAN bus will not communicate. The PFMEA should identify this as a failure mode with a detection method that includes a pin-to-pin verification against the released pinout, not just a generic continuity check.
Crimp Height Drift During Production
Crimp height on 22 AWG wire is a window measured in tenths of a millimeter. If the crimp applicator drifts 0.05 mm over a 5,000-piece run, the pull force can drop below the minimum specification. The control plan should specify crimp height checks at a defined interval, typically every 500 crimps or at the start of each shift, with the data recorded in a setup verification log.
Shield Drain Wire Termination Failure
On shielded OBD assemblies, the drain wire is often the smallest conductor in the bundle. If it is crimped into the same terminal as a signal wire, the crimp may not capture both conductors reliably. The PFMEA should flag this as a distinct failure mode, with a detection method that includes a visual inspection of the drain wire seating before the overmold process.
A harness factory running IATF 16949 systems for years will treat the PFMEA as a living record. When a new terminal is introduced, when the wire supplier changes, or when the overmold tool is replaced, the PFMEA is updated with a revised severity, occurrence, and detection rating. A Level 3 submission should include the PFMEA revision history page, not just the current version. For more on how that system works in practice, see this IATF 16949 certification overview.
Control Plan: Where the PFMEA Becomes a Daily Check
The control plan is where the PFMEA becomes a daily check. For a 16-pin OBD cable, it should name the check, the frequency, the tool, and the reaction when the check fails. If the crimp height check says “every 500 crimps” but the reaction plan says “notify supervisor,” that is not a control plan. It is a suggestion.
Production-Intent Control Plan Checks
A production-intent control plan for a 16-pin OBD assembly typically includes these checks:
| Process Step | Characteristic | Specification | Sample Size | Frequency | Control Method | Reaction Plan |
| Wire cut | Length | Plus or minus 2.0 mm | 5 pieces | Every 500 pieces | Automated cutter with length log | Stop, recalibrate, quarantine since last check |
| Crimp | Crimp height | Per setup card | 5 pieces | Every 500 crimps | Micrometer, recorded | Stop, re-set applicator, re-verify |
| Crimp | Pull force | 50 N minimum, 22 AWG | 5 pieces | Setup plus every 2,000 | Pull tester | Stop, inspect all since last good pull test |
| Insertion | Terminal seating | Flush to cavity shoulder | 100 percent | Every unit | Visual plus tactile click check | Rework or scrap |
| Electrical | Continuity and pinout | Per released pinout | 100 percent | Every unit | Automated tester, such as Cirris | Quarantine, investigate tester and fixture |
| Final | Overmold flash | 0.15 mm maximum | 10 pieces | Every hour | Visual plus pin gauge | Adjust mold, inspect since last check |
100 Percent Continuity Test Requirement
The 100 percent continuity test row is the one that separates a serious harness supplier from a broker. An OBD cable has 16 potential contact points. A continuity test that checks only for opens misses crossed wires and intermittent high-resistance connections. The test fixture must verify the full pin-to-pin map against the released engineering pinout, with a resistance threshold of 2 ohms or less for signal lines and a separate threshold for power and ground. The test data, pass or fail per unit, with a timestamp and serial number, should be retained and traceable to the production lot. For higher-voltage insulation resistance checks, the continuity 500VDC IR testing CAN bus failures method is a useful reference. Moisture ingress can also show up as pin-to-pin leakage, which is why the moisture ingress pin-to-pin leakage current test belongs in the qualification plan for underhood and wet-bay applications.
What Crimp Cpk Is Required for OBD Cable Assemblies?
The initial process study section of a Level 3 PPAP is where the supplier demonstrates that the production process is capable, not just that the sample passed. For an OBD cable assembly, the critical process capability study is crimp height Cpk.
Crimp height is a special characteristic because it directly controls pull force, which in turn controls connector reliability. A capable crimp process typically shows a Cpk of 1.33 or higher on crimp height. If the Cpk is below 1.00, the process is not capable. It is producing parts that will drift out of specification as the applicator wears. Crimp height also sets crimp resistance; a 3.2 milliohm drift can be enough to create a ground offset, as this crimp resistance drift J1939 ground offset case shows.
Crimp Height Capability Study Data
Here is what a crimp height capability study looks like in a real submission:
- Sample size: 30 consecutive crimps from a single setup, collected after the applicator has reached thermal equilibrium, typically after 50 to 100 crimps.
- Measurement: Crimp height measured with a calibrated micrometer or a crimp height comparator.
- Data: Raw measurements listed in the submission, not just the calculated Cpk.
- Control chart: An X-bar and R chart showing the measurements plotted against the specification limits, with the average and range control limits calculated from the data.
Pull-Force Capability and Real Case
For pull force, the capability study is often destructive. The crimp is pulled until it fails. The data from 25 pull tests, per USCAR-21 minimum, is used to calculate the minimum pull force and confirm that it exceeds the specification with margin. If the lowest pull force in the sample is 48 N against a 50 N specification, the process is not capable, even if the average is 75 N.
A real case from a custom OBD program shows why this matters. The assembly used a 16-pin J1962 connector, 20 AWG power and ground, and 22 AWG CAN lines. The first-run crimp height Cpk was 1.08. The pull force average was acceptable, but the minimum reading was 47 N against a 50 N minimum. The applicator was rebuilt, the crimp height was re-set, and the second study produced a Cpk of 1.52. Because the first run had already produced 800 cables, the factory re-tested every cable for pull force and continuity before shipping. The PPAP was approved, but only after the process evidence matched the production reality.
Measurement System Analysis: The Document Buyers Ask For and Suppliers Forget
When a dimensional report looks too clean, I ask for the Gage R&R. On a 22 AWG crimp with a plus or minus 0.05 mm window, operator variation of 0.03 mm eats more than half the tolerance. At that point, the crimp process may be capable, but the measurement system is hiding it.
A Gage R&R study for an OBD cable assembly typically covers two measurement systems.
Crimp Height Measurement
If the crimp height is measured with a handheld micrometer, the MSA must show that the measurement variation between three operators is less than 10 percent of the tolerance window. If the tolerance is plus or minus 0.05 mm and the operator variation is 0.03 mm, the measurement system is consuming more than half the tolerance. The SQE will question whether the crimp process is actually capable.
Pull-Force Tester
The pull-force fixture must have a calibration certificate traceable to a national standard. The MSA should include a linearity study across the expected force range, for example from 20 N to 150 N, to confirm that the load cell reads accurately at both the low and high ends of the specification.
Level 3 does not always require MSA on paper. In practice, if the crimp height report shows a Cpk of 1.45 but no Gage R&R, the SQE will assume the measurement system was not validated. That assumption delays approval.
Material, RoHS, REACH, and Performance Records: What Has to Trace Back to the Lot
For a custom OBD cable assembly, the material test records are not about the copper inside the wire. They are about the connector housing, the terminal plating, the overmold compound, and the label adhesive. Each of these has a specification, and each specification has a test method.
Material and Performance Records Checklist
A complete material and performance section for a Level 3 submission includes:
- Connector housing material certificate. PBT or PA66 with a UL 94 V-0 flammability rating. The certificate of analysis must trace to the lot number used in the sample build. For jacket thickness and flex tradeoffs, see this UL 94 V-0 diagnostic cable jacket thickness flex note.
- Terminal plating thickness report. Gold flash over nickel, or tin plating, depending on the circuit. The report should include X-ray fluorescence measurements at three points per terminal lot.
- Overmold compound data sheet. If the assembly uses a PVC or TPE overmold, the data sheet must confirm the operating temperature range and the dielectric strength. For underhood applications, the overmold material may also need to meet a fluid resistance specification.
- RoHS and REACH compliance declaration. Not a supplier promise. A test report from a qualified laboratory, with the sample date and the laboratory accreditation number.
- Performance test results. For an OBD cable assembly, the performance tests that matter are insertion and withdrawal force per SAE J1962, cable retention force per USCAR-21 or equivalent, and, if the assembly is shielded, a shield continuity and transfer impedance test.
The RoHS and REACH documentation is where many Chinese harness suppliers fall short on their first submission. A declaration that says “our products comply with RoHS” is not evidence. The SQE wants a test report, typically from an ISO/IEC 17025-accredited laboratory, that shows the measured levels of lead, cadmium, mercury, hexavalent chromium, PBB, and PBDE against the RoHS thresholds. For REACH, the SVHC declaration must be current against the latest candidate list.
A factory that uses a full-plastic design, meets RoHS standards, and tests 100 percent of cables will have this data on file. It should be pulled by lot number, not written from memory.
Qualified Laboratory Documentation: The Evidence an SQE Cannot Generate
The lab documentation section of a Level 3 PPAP is the part that the SQE cannot verify through inspection. They cannot look at a cable assembly and know whether the overmold material passed the flammability test, or whether the terminal plating meets the corrosion resistance specification. They depend on the laboratory reports in the submission.
Required Laboratory Reports for OBD Cable Assemblies
For an OBD cable assembly, the qualified lab documents typically include:
- Flammability test report for the connector housing and overmold material, per UL 94 or an equivalent standard.
- Salt spray corrosion test for the terminal plating, per ASTM B117 or an OEM-specific standard. For underhood applications, a 96-hour salt spray exposure with no base metal corrosion is a common requirement.
- Thermal shock test if the assembly is rated for temperature cycling. The report should show the temperature range, the number of cycles, and the post-test electrical continuity results.
- Vibration test if the assembly is mounted in a high-vibration location, such as near the engine or transmission.
The lab reports must come from a laboratory that is either accredited to ISO/IEC 17025 or recognized by the OEM’s supplier quality organization. A report from an in-house lab is acceptable only if the lab has a documented quality system and the test equipment is calibrated. The SQE will check the calibration certificate for the test equipment listed in the report.
Factories that also provide salt spray testing in-house can shorten the loop, but the report still needs calibration records and a controlled test method. The point is not who runs the test. The point is whether the evidence can survive an audit.
Part Submission Warrant: A Warranty, Not a Cover Page
The PSW is usually one page. It is also the page that gets the supplier in trouble. If the sample was built on Crimp Setup 001 and the production control plan names Setup 004, the signature is not an approval. It is a process mismatch waiting to be found.
What the PSW Must Specify
For a custom OBD cable assembly, the PSW should specify:
- The customer part number and the supplier part number.
- The engineering drawing revision level.
- The date of the sample build and the production date range for the PPAP run.
- The number of samples submitted and the lot traceability information for the wire, terminals, and connector housings used.
- The submission level, Level 3 in this case, and the disposition: approved, interim approval, or rejected.
The PSW is a warranty. If the sample build used a different terminal than the production control plan calls out, the signature is not an approval. It is a liability. When the OEM finds the mismatch, the approval is revoked and the supplier’s quality rating takes the hit. That is why a revision lock before submission is cheaper than a re-submission after a field failure. For a deeper look at traceability, see this IATF 16949 cable assembly traceability guide.
A Realistic PPAP Level 3 Timeline for a Custom OBD Cable
A Level 3 PPAP for a custom OBD cable assembly is not a one-week exercise. From the time the drawing is released, a realistic timeline looks like this:
PPAP Level 3 Timeline Table
| Week | Activity | Output |
| 1 to 2 | Design review, ballooned drawing, BOM lock | Released drawing with balloon numbers |
| 2 to 3 | PFMEA and control plan drafting | Draft PFMEA and control plan aligned to flow diagram |
| 3 to 4 | Tooling and fixture build, crimp setup | Crimp applicator set, test fixture validated |
| 4 | First-article build and dimensional inspection | Dimensional report with raw data |
| 4 to 5 | Crimp capability study, pull-force testing | Cpk data, pull-force data |
| 5 | MSA, Gage R&R on crimp height and pull tester | MSA report |
| 5 to 6 | Material and performance testing, external lab | Lab reports |
| 6 | PSW preparation and package assembly | Complete Level 3 submission |
If the factory already runs the same terminal family and has a Cirris fixture programmed for the 16-pin J1962 map, the PPAP can move in three to four weeks. If the connector is new or the overmold tool has to be built, six to eight weeks is realistic. If the lab testing reveals a material failure, the timeline restarts at the material change.
What to Ask Your Supplier Before They Submit a PPAP
If you are sourcing a custom OBD cable assembly and the supplier will be submitting a Level 3 PPAP, these questions reveal whether the submission will be credible:
Six Supplier Questions Before PPAP Submission
- Can you provide a ballooned drawing before the dimensional report? If the supplier measures dimensions without a ballooned drawing, the data is not traceable to the drawing.
- What is the crimp height Cpk on the terminal and wire gauge you used for the sample? A supplier who cannot answer this question has not run a capability study.
- Can you show me the pull-force data for every populated cavity, not just the average? A single pull-force number is not evidence.
- Is the RoHS and REACH test report from an accredited laboratory, and is it current? A declaration letter is not a test report.
- What is the revision level of the control plan compared to the drawing on the PSW? If they cannot answer immediately, the package has a revision mismatch.
- Does the continuity test fixture verify the full pin-to-pin map, or just opens and shorts? A generic continuity test will not catch mis-pinned CAN lines.
If the supplier needs three days to answer the crimp Cpk question, the PPAP is probably being assembled from documents, not from the process. Ask for the raw data behind the number.
Why OBD Cable Assemblies Are Harder Than Standard Harnesses
A standard wire harness with a connector on each end has a straightforward PPAP: measure the length, verify continuity, check the crimp height. An OBD cable assembly adds three layers of complexity that make the PPAP more demanding.
Defined Connector Interface
The connector is a defined interface. SAE J1962 specifies the connector envelope, the terminal position, and the insertion and withdrawal force. The cable assembly must meet those specifications, not just fit the mating connector on a bench test.
Stricter Signal Integrity
The signal integrity requirements are stricter. CAN bus lines operate at differential voltages with defined termination impedances. A crimp that adds 0.5 ohms of resistance may pass a continuity test but degrade the CAN signal at high data rates. The test protocol for a CAN-enabled OBD cable should include a resistance measurement on the CAN lines, not just a continuity check. For bench work where a 50 MHz scope misses fast glitches, see why 50 MHz scope misses CAN bus glitches.
Repeated Handling
The cable is handled repeatedly. A diagnostic cable is plugged and unplugged multiple times in its service life. The insertion and withdrawal force specification and the strain relief design have to account for 10,000 cycles or more, depending on the application. The PPAP should include a durability test result, even if it is a bench-top cycling test on the sample, to show that the design has been validated beyond the first insertion.
Frequently Asked Questions
Can a PPAP Level 3 submission be done without a ballooned drawing?
No. The ballooned drawing is the reference document for the dimensional report. Without it, the SQE cannot verify that each measured dimension corresponds to a drawing callout. A dimensional report without a ballooned drawing is a list of measurements, not a dimensional inspection.
What is the most common reason a Level 3 PPAP for a cable assembly is rejected?
Revision mismatch. The sample, the PSW, the dimensional report, and the control plan reference different drawing or BOM revisions. This is the most common and the most avoidable rejection reason. A revision lock process before submission prevents it.
How many samples are required for a Level 3 PPAP?
The PPAP manual does not specify a fixed number for Level 3. In practice, the sample quantity is defined by the customer’s submission requirement. For a cable assembly, three to five production-intent samples are typical, with the dimensional data reported for each sample. The samples should come from a production run, not from a prototype build.
Does a custom OBD cable assembly need IATF 16949, or is ISO 9001 sufficient?
For safety-critical or underhood applications, IATF 16949 is typically required. For diagnostic cables used in a service bay or test bench application, ISO 9001 may be acceptable, depending on the OEM’s supplier requirements. However, an IATF 16949-certified factory will have the PPAP and APQP systems already in place, which makes the Level 3 submission faster and more reliable.
What is the difference between a Level 3 and a Level 4 PPAP for cable assemblies?
Level 3 requires the PSW, samples, and complete supporting data submitted to the customer. Level 4 requires the PSW and any other requirements the customer defines. It does not automatically include the full supporting package. Level 3 is the default for new production harness programs. Level 4 is sometimes used for prototype or low-volume builds.
How long does PPAP approval typically take?
If the submission is complete and the data supports approval, the customer’s SQE can approve within one to two weeks. If the submission requires clarification or additional testing, the timeline extends to four to six weeks or longer. The most common cause of delay is not a quality problem. It is an incomplete package that requires the supplier to re-submit missing or corrected documents.
Can a supplier submit a PPAP without a Gage R&R study?
Technically, MSA is required only for variable measurement systems on special characteristics. In practice, for crimp height and pull-force measurements on a safety-related circuit, the SQE will expect an MSA. A submission without MSA data will likely receive an interim approval with a request for the MSA before final approval.
What happens if the PPAP is approved but the production parts do not match the sample?
If the production parts do not match the approved sample, the PPAP approval is not valid. The supplier is required to notify the customer of any change in process, material, or sub-supplier that could affect the product. Shipping parts that do not match the approved PPAP is a nonconformance that can lead to a supplier corrective action request, or SCAR, and a re-submission of the PPAP.
How does the factory verify 100 percent continuity on every OBD cable?
The factory uses an automated cable tester, typically a Cirris, CableEye, or equivalent system, programmed with the released pinout. The tester checks every circuit for opens, shorts, and mis-wires. The test result, with a timestamp and unit serial number, is logged and traceable to the production lot. For a 16-pin OBD assembly, the test verifies all populated circuits against the engineering pinout.
What RoHS and REACH documents should be included in the PPAP?
A test report from an ISO/IEC 17025-accredited laboratory showing the measured levels of the RoHS-restricted substances against the thresholds. For REACH, a current SVHC declaration against the latest candidate list. A supplier declaration letter is not a substitute for a test report.
Working With a Factory That Treats PPAP as Process Evidence
The difference between a PPAP submission that gets approved and one that sits in review is not the thickness of the package. It is whether the documents tell a consistent story about the process.
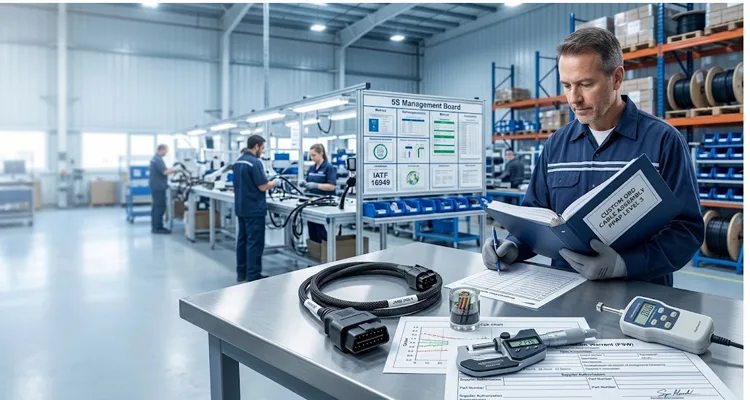
A factory that has been running IATF 16949 and ISO 9001 systems for years, with 5S management, climate-controlled warehousing for temperature-sensitive materials, and a four-step quality inspection process from incoming material to final test, does not treat PPAP as a special project. It treats it as the normal way of launching a new program. That factory is also more likely to hold ISO 14001, RoHS, CE, UL, and REACH certifications because those systems are already part of how it operates. The ISO 14001 side of that system matters when overmold compounds, plating chemistry, and waste streams have to be controlled alongside product quality.
If you are sourcing a custom OBD cable assembly and you need a PPAP Level 3 package that reflects a real production process, bring the drawing and the PPAP element list to the engineering team. Sales can quote the cable. Engineering has to prove the crimp setup, test fixture, and MSA can support a Level 3 submission. The factory should support OEM customization for logo, brand, length, color, and AWG, and it should be able to show 20 plus years of direct factory experience, not a trading company’s document set.
You can reach the engineering team through the Contact page for a technical review of your drawing and PPAP requirements, or through WhatsApp for a faster response on urgent program timelines. If your program requires a Level 3 PPAP, the first step is a drawing review, and that starts with a conversation about the design record, not the price.
